Excavator bucket teeth are the cutting and penetration components mounted at the front of excavator, loader and dredging buckets. They bear direct contact with soil, rock and mineral aggregates, enduring extreme impact and abrasive wear. Material selection determines whether a tooth maintains penetration efficiency over hundreds of hours or dulls within days. This guide covers three wear-material options for bucket teeth — high-manganese Hadfield steel (110Г13Л), alloy steel (30CrNiMo), and boron-alloyed steel — and the forged-versus-cast decision, as part of our broader washing, conveying and fluid engineering wear-parts program. For the teeth themselves — GP/HD/XD styles, material properties and quotes — see our cast bucket teeth product page.
What Are Excavator Bucket Teeth and Why Material Matters
Bucket teeth are the replaceable cutting tips on the leading edge of excavator, loader and dredging buckets. They are the direct interface between the machine and the excavated material — soil, clay, gravel, broken rock or concrete. The tooth must penetrate the material efficiently, resist impact fracture when striking hard obstacles, and resist abrasive wear as material flows across its surface. The failure mode depends on the application: in earthmoving, gradual abrasive wear dulls the tip; in quarry and mining, hard-rock impacts chip and fracture the cutting edge; in demolition, concrete and rebar impose combined impact and shear loads. No single material is optimal for all duties — the selection problem is matching the alloy’s hardness, toughness and self-sharpening behavior to the specific application and operating conditions.
Bucket Tooth Materials at a Glance
| Material | Initial Hardness | Work-Hardened Hardness | Impact Toughness (KCV) | Typical Duty |
|---|---|---|---|---|
| 110Г13Л Hadfield steel | HB 180–220 | HB 400–500 | ≥ 80 J/cm² | High-impact earthmoving |
| 30CrNiMo alloy steel | HRC 45–55 (core) | HRC 55–65 (surface) | 20–40 J/cm² | Hard-rock penetration |
| Boron-alloyed steel | HRC 50–55 | HRC 55–65 | 15–25 J/cm² | Medium-impact + high wear |
Tensile strength ≥ 750 MPa (110Г13Л, ГОСТ 2176). Tooth types: GP (general purpose), HD (heavy duty), XD (extra heavy duty). Mounting: two-piece (adapter + replaceable tip) or one-piece. Compatible with CAT, Komatsu, Hitachi, Volvo and other mainstream equipment.
110Г13Л Hadfield Steel: The Self-Hardening Grade
110Г13Л — the Russian designation for Hadfield steel (Mn 10–14%, C 1.0–1.3%) — is the standard material for high-impact bucket teeth. In its as-heat-treated condition it is relatively soft (HB 180–220), but its defining property is work hardening: under impact loading, the surface hardness rises to HB 400–500 while the core retains high toughness. The tooth becomes harder the harder it works — the more rock it strikes, the more wear-resistant its surface becomes. With impact toughness ≥ 80 J/cm² (KCV, V-notch, per ГОСТ 977/2176), it does not brittle-fracture at –40°C, making it the safest choice for high-impact applications in cold climates. The trade-off: without sufficient impact, the surface does not work-harden effectively, and the low initial hardness means faster wear in purely abrasive conditions.
30CrNiMo Alloy Steel: The Hard-Rock Penetration Grade
For hard-rock penetration where surface hardness must be high from the start, 30CrNiMo-class alloy steel is the optimum choice. Through carburizing or surface quenching, the surface reaches HRC 55–65 while the core remains at HRC 45–55 — a controlled hardness gradient that combines a sharp, wear-resistant cutting edge with a tough, fracture-resistant core. Unlike Hadfield steel, this hardness is built in from day one — no work-hardening needed — making it the better choice for applications with high abrasive wear but moderate impact. Impact toughness is 20–40 J/cm², lower than Hadfield steel, so it is not suited for extreme-impact loading or severe sub-zero temperatures. In quarry and mining duty, the higher surface hardness and self-sharpening tooth geometry maintain penetration force as the tooth wears, delivering 2–4 times the service life of ordinary carbon steel.
Boron-Alloyed Steel: The Cost-Effective Mid-Duty Grade
Boron-alloyed steel (low-carbon steel with boron micro-alloying) occupies the cost-performance middle ground. With HRC 50–65 hardness, it delivers wear resistance comparable to alloy steel at lower cost — the small boron addition replaces more expensive chromium and molybdenum while achieving similar hardenability. Impact toughness is 15–25 J/cm² — the lowest of the three options — so it is not suitable for heavy-impact or extreme-cold applications. Its niche is medium-impact, high-wear conditions where cost control matters: general earthmoving with abrasive soils, sand and gravel loading, and auxiliary bucket positions where replacement is straightforward. Service life is 2–3 times that of ordinary carbon steel, with moderate self-sharpening effect.
Selection Summary by Application
- Earthmoving (general soil excavation): 110Г13Л GP — self-hardening + low-temperature toughness, ≥ 80 J/cm².
- Quarry and mining (hard-rock penetration): 30CrNiMo HD/XD — high surface hardness from day one + hardness gradient.
- Sand and gravel loading: 110Г13Л GP — impact hardening from material flow.
- Dredging (underwater mud and sand): 110Г13Л + anti-corrosion treatment — work-hardening plus corrosion protection.
- Building demolition (concrete and rebar): 30CrNiMo XD — combined impact and shear resistance.
- Medium-impact high-wear (cost-sensitive): Boron-alloyed steel — adequate hardness at lower material cost.
Performance vs Ordinary Carbon Steel
Compared with ordinary carbon-steel bucket teeth (HB 200–250, no self-sharpening), all three material options deliver significant life improvements. Hadfield steel delivers 3–5 times the service life, with self-sharpening performance rated good — the tooth maintains a sharp cutting edge through work-hardening as it wears. Alloy steel delivers 2–4 times, also with good self-sharpening through V-taper tooth geometry. Boron-alloyed steel delivers 2–3 times with moderate self-sharpening. The critical difference from carbon steel is penetration-force maintenance: carbon steel dulls progressively as it wears, increasing fuel consumption and reducing productivity, while Hadfield and alloy steel teeth maintain penetration through self-sharpening geometry. At –40°C, Hadfield steel retains excellent toughness (no brittle fracture), while carbon steel and boron steel are rated medium.
Casting, Forging and Quality Control
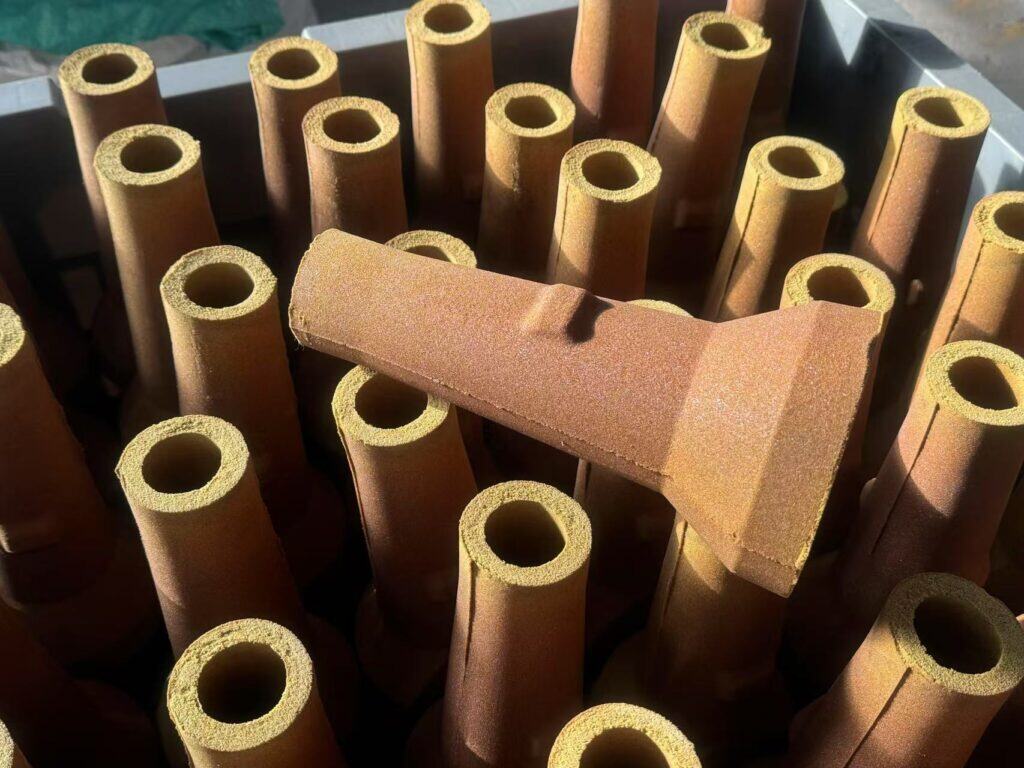
High-manganese Hadfield steel bucket teeth must be cast — the work-hardening property that makes the material excellent in service also makes it nearly impossible to machine, so precision casting is the only viable production route. Alloy steel teeth can be either forged or cast; forging improves grain-flow continuity and fatigue strength, but for complex tooth geometries with self-sharpening profiles, precision casting with subsequent heat treatment delivers comparable performance at lower cost. The production process: medium-frequency induction-furnace melting with strict Mn/C ratio control for Hadfield steel and Cr/Ni/Mo ratio control for alloy steel; precision casting to ensure tip geometry and self-sharpening profile accuracy; heat treatment — water toughening (solution treatment) for Hadfield steel to retain austenite structure, carburizing/surface quenching plus tempering for alloy steel to achieve the hardness gradient.
Quality control includes spectroscopic composition analysis, hardness-gradient testing (surface to core), impact-toughness testing, and full dimensional inspection. Adapter interface dimensions are precision-machined to match equipment bucket mounting seats. ISO 9001 quality system throughout; material and test reports available; supports ГОСТ compliance requirements (including ГОСТ 2176-77 for high-manganese steel castings).
Why Huasuma for Excavator Bucket Teeth
Huasuma’s metal casting capability covers three bucket-tooth material options — 110Г13Л Hadfield steel, 30CrNiMo alloy steel and boron-alloyed steel — with GP, HD and XD tooth types matched to the application. The self-sharpening design depends on non-symmetric cross-section material distribution: casting deviation causes the sharp edge to fail during wear, and penetration force drops rapidly. Precision casting plus dimensional inspection ensures each tooth’s self-sharpening profile meets the designed geometry. For Hadfield steel, the water-toughening process strictly controls austenite retention — improper treatment causes carbide precipitation and toughness loss, and Huasuma’s heat-treatment procedure ensures the work-hardening characteristic performs as designed. Equipment-brand compatibility covers CAT, Komatsu, Hitachi and Volvo by equipment model. With 30 years of casting export experience and multiple batches delivered to Russian, Indian and Australian construction-machinery clients, this is proven production. ISO 9001 throughout; 24-hour quote response; samples available for in-service validation before bulk orders.
FAQ
What is the best material for excavator bucket teeth?
It depends on the application. For high-impact earthmoving, 110Г13Л Hadfield steel — its work-hardening property raises surface hardness to HB 400–500 under impact, with ≥ 80 J/cm² impact toughness and no brittle fracture at –40°C. For hard-rock quarry and mining, 30CrNiMo alloy steel — HRC 55–65 surface hardness from day one with a tough HRC 45–55 core.
What is the difference between forged and cast bucket teeth?
High-manganese Hadfield steel (110Г13Л) must be cast — its work-hardening property makes machining nearly impossible. Alloy steel teeth can be forged or cast; forging improves grain-flow continuity and fatigue strength, but for complex tooth geometries with self-sharpening profiles, precision casting with surface heat treatment delivers comparable wear performance at lower cost. The forged-versus-cast decision is secondary to material selection — the right alloy for the right application matters more than the forming process.
How long do excavator bucket teeth last?
Hadfield steel teeth deliver 3–5 times the service life of ordinary carbon steel; alloy steel 2–4 times; boron-alloyed steel 2–3 times. Actual hours depend on the material being excavated, operating conditions and tooth type (GP/HD/XD). Hadfield and alloy steel teeth maintain penetration force through self-sharpening, while carbon steel dulls progressively.
Do Huasuma bucket teeth fit CAT, Komatsu and Hitachi equipment?
Yes — the two-piece adapter + replaceable tip system is compatible with CAT, Komatsu, Hitachi, Volvo and other mainstream equipment. Custom-fit by equipment model, with adapter interface dimensions precision-machined to match the specific bucket mounting seat.
Huasuma is a Chinese manufacturer of excavator bucket teeth in 110Г13Л Hadfield steel, 30CrNiMo alloy steel and boron-alloyed steel. Self-sharpening design, GP/HD/XD types, compatible with CAT, Komatsu, Hitachi and Volvo. Supplied worldwide. Request a quote or sample.