Double roll crusher segments — the wear-resistant rollers at the heart of 2PG series double roll crushers — take the full force of hard rock being pulled between two counter-rotating rolls. Traditional high manganese steel segments start at only HB 179–219 in the cast state and require strong impact to work-harden; in medium-to-low impact duty they never reach effective hardness, wear fast and need frequent replacement. High-chrome white cast iron segments (KmTBCr15 / KmTBCr20 / KmTBCr26) deliver HRC 58–65 as a factory-final hardness — no work-hardening needed — with 1.5 times the service life of manganese steel and 30% lower overall cost. This guide covers the material grades, selection criteria and quality control for double roll crusher segments, as part of our broader mining, crushing and aggregate processing wear-parts program. See our crusher wear parts catalog for the full jaw, cone and impact range.
What Are Double Roll Crusher Segments and Why Material Matters
Double roll crusher segments are the wear-resistant roller surfaces fitted to 2PG-400, 2PG-610, 2PG-750 and 2PG-900 series double roll crushers. When processing limestone, iron ore, granite and other hard rock (compressive strength 60–200 MPa), the roll surface takes high-frequency impact combined with sliding wear — material is compressed between the rolls and sheared as it passes through the gap. The failure mode is surface wear from abrasive sliding plus impact pitting. The material problem is that high manganese steel, the traditional choice, depends on strong impact to work-harden; in double roll crushing the impact is often medium-to-low, so manganese segments stay soft and wear rapidly. High-chrome white cast iron solves this by delivering HRC 58–65 as the final heat-treated hardness, independent of in-service work-hardening. The selection problem is matching the chromium level (Cr15 / Cr20 / Cr26) to the material hardness and impact energy.
High-Chrome Cast Iron Segment Grades at a Glance
| Grade | Cr content | Hardness (HT) | Impact toughness | Typical duty |
|---|---|---|---|---|
| KmTBCr15 | 14–18% | HRC 58–65 | ≥ 15 J/cm² | Limestone, medium-hard rock |
| KmTBCr20 | 18–23% | HRC 58–65 | ≥ 15 J/cm² | Iron ore, high-impact balance |
| KmTBCr26 | 23–28% | HRC 60–65 | ≥ 15 J/cm² (HT-guaranteed) | Extreme wear, high-hardness rock |
Density: 7.2–7.5 g/cm³. Core chemistry: C 2.4–3.0%, Cr 14–28% depending on grade. Casting: coated-sand precision casting (small/medium segments) or lost-foam casting (large segments). Pouring temperature: 1380–1420°C. Hardness tested at 3 points per piece, HRC 58–65 as factory gate.
KmTBCr15: The Limestone and Medium-Hard Rock Grade
KmTBCr15 (14–18% chromium) is the entry grade of high-chrome white cast iron for double roll segments, suited to limestone and medium-hardness aggregate where wear is moderate but impact is not extreme. After quench-and-temper heat treatment it reaches HRC 58–65 — already three times the hardness of manganese steel in the cast state (HB 179–219). Its advantage is the combination of good wear resistance with the highest toughness in the KmTBCr series, making it the most crack-resistant option for duties where impact is variable. For limestone crushing in aggregate and sand production, KmTBCr15 provides the best balance of wear life and cost. The limitation is that for high-hardness rock or extreme wear conditions, Cr15’s wear resistance is exceeded by the higher-chromium grades.
KmTBCr20: The Balanced High-Wear Grade
KmTBCr20 (18–23% chromium) is the balanced grade for high-wear duty combined with medium impact — iron ore processing, high-hardness aggregate and manufactured sand production. The higher chromium content increases the volume of hard M₇C₃ carbides in the matrix, raising wear resistance above Cr15 while maintaining impact toughness at ≥ 15 J/cm². For iron ore and high-impact hard rock in double roll crushers, KmTBCr20 is the standard choice — it provides the wear life needed without the cost premium of Cr26. The heat treatment parameters differ from Cr15: the quench-and-temper cycle is tuned to optimize carbide morphology and toughness for the higher chromium level, ensuring the M₇C₃ carbides form as isolated rods rather than a continuous network that would embrittle the segment.
KmTBCr26: The Extreme-Wear Grade
KmTBCr26 (23–28% chromium) is the top wear-resistance grade for extreme-wear duty with high-hardness materials. With the highest chromium content, it produces the greatest volume of hard M₇C₃ carbides, delivering HRC 60–65 and the best abrasive wear resistance in the series. The trade-off is that higher carbide volume reduces toughness, so Cr26’s impact toughness must be guaranteed through heat treatment — the quench-and-temper parameters are specifically designed to control carbide morphology and prevent the brittleness that traditionally plagued high-chrome cast iron. This grade is specified for the most abrasive materials and the most demanding double roll applications where segment life is the priority and impact is moderate enough that toughness can be heat-treatment-guaranteed rather than inherent.
Selection Summary by Application
- Limestone / medium-hard aggregate (2PG series): KmTBCr15 — best toughness, cost-effective, HRC 58–65.
- Iron ore / high-hardness aggregate: KmTBCr20 — balanced wear resistance and toughness, ≥ 15 J/cm².
- Extreme-wear, high-hardness rock: KmTBCr26 — maximum wear resistance, HRC 60–65, toughness heat-treatment-guaranteed.
- Medium-to-low impact duty: Always high-chrome cast iron over manganese steel — manganese cannot work-harden effectively in low-impact conditions.
- Custom roll dimensions: Roll diameter, roll length and shaft bore machined to customer drawings for any 2PG model.
Performance: High-Chrome Cast Iron vs High Manganese Steel
Compared with high manganese steel (Mn13Cr2, cast hardness HB 179–219), high-chrome white cast iron segments deliver HRC 58–65 as the factory-final hardness — more than three times higher, with no dependence on in-service work-hardening. In the medium-to-low impact conditions typical of double roll crushing, where manganese steel never reaches effective hardness, high-chrome segments wear at only 60–70% of the rate of manganese steel. Field data from customer operations confirms: service life is 1.5 times that of manganese steel segments, replacement frequency is reduced by 40%, and overall cost (including replacement frequency and downtime) is reduced by approximately 30%. The critical advantage is that high-chrome cast iron is hard from the start — there is no “break-in” period during which the segment wears rapidly while waiting to harden.
Casting Process and Quality Control
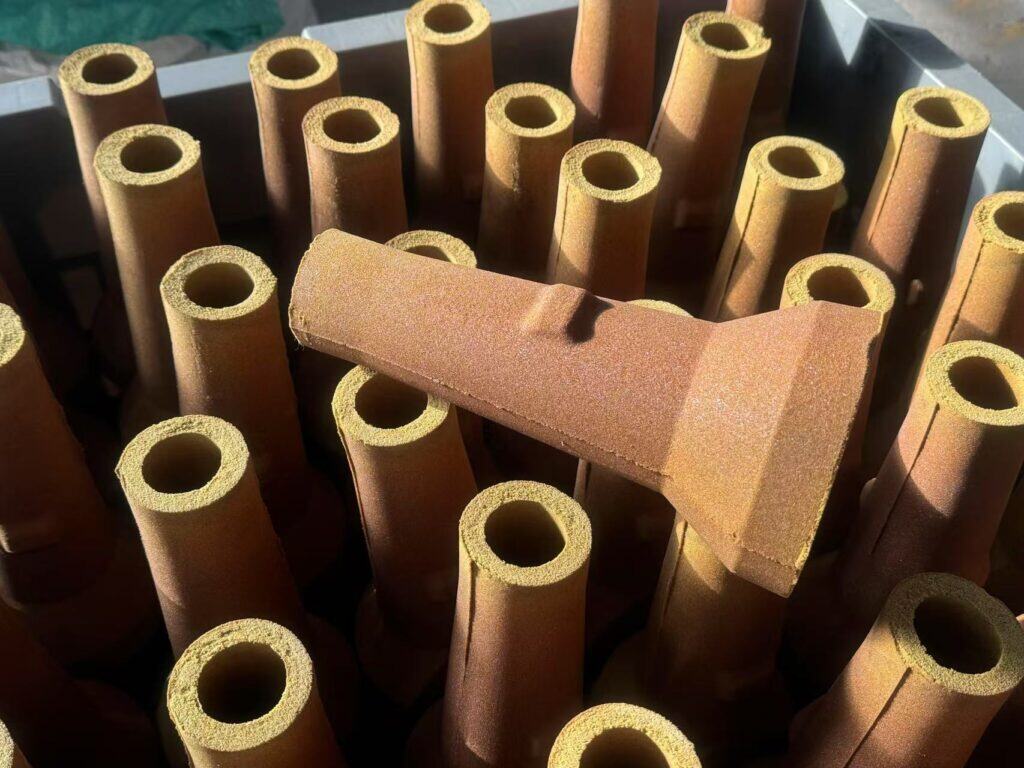
Double roll segments are produced by coated-sand precision casting (small and medium segments) or lost-foam casting (large segments), with pouring temperature 1380–1420°C. The pre-pour “double rule” — furnace-front temperature measurement plus sample-block chemistry check — ensures chemical composition meets specification before pouring. Heat treatment is a quench-and-temper dual process: quenching optimizes the carbide morphology from the brittle network M₃C form to the isolated rod-like M₇C₃ form, and tempering eliminates internal stress to guarantee toughness. Each grade (Cr15 / Cr20 / Cr26) uses independent quench-and-temper parameters to optimize the hardness-toughness balance for its chromium level.
Quality control includes 100% hardness testing on every piece (3 points per segment, HRC 58–65 as factory gate), ultrasonic flaw detection sampling for internal defects, metallographic analysis to confirm M₇C₃ carbide morphology as the target structure, and full traceability. ISO 9001 quality system throughout; material and test reports available. Supports GOST compliance requirements.
Why Huasuma for Double Roll Crusher Segments
Double roll segments are the core wear part of the crushing equipment, and their performance depends on high-chrome cast iron composition control, heat treatment parameters and carbide morphology — requirements far higher than for ordinary cast iron or cast steel. Huasuma’s metal casting capability offers three grades (KmTBCr15 / Cr20 / Cr26), each with independent quench-and-temper parameters — limestone duty uses Cr15 for economy, iron ore duty uses Cr26 for maximum life; not one formula for all duties. Quenching transforms the carbide morphology from network M₃C to isolated M₇C₃ — confirmed by metallographic analysis on every piece, a verifiable test result. Pre-pour double rule (furnace-front temperature + sample chemistry), 100% hardness testing (3 points per piece, HRC 58–65 gate), ultrasonic inspection and metallographic analysis. ISO 9001 throughout; supports GOST compliance; material reports, test reports and hardness distribution charts available. With 30 years of high-chrome cast iron wear-part manufacturing experience, 10,000+ tons annual capacity, and multiple batches delivered to Russian, Indian and Australian customers, this is a proven large-scale supply chain — not sample trials. 24-hour quote response; samples available for in-service validation before bulk orders.
FAQ
Why is high-chrome cast iron better than manganese steel for double roll segments?
High-chrome white cast iron reaches HRC 58–65 as the factory-final hardness after heat treatment — over three times the cast hardness of manganese steel (HB 179–219). Manganese steel depends on strong impact to work-harden, but double roll crushing often produces only medium-to-low impact, so manganese segments stay soft and wear rapidly. High-chrome segments are hard from the first day, wear at 60–70% of the manganese rate, and deliver 1.5 times the service life with 30% lower overall cost.
What is the difference between KmTBCr15, Cr20 and Cr26?
Chromium content and wear resistance. Cr15 (14–18% Cr) is the toughest and most economical, suited to limestone and medium-hard rock. Cr20 (18–23% Cr) balances higher wear resistance with toughness for iron ore and high-hardness aggregate. Cr26 (23–28% Cr) delivers maximum wear resistance (HRC 60–65) for extreme-wear duty, with toughness guaranteed through heat treatment. Each grade has its own quench-and-temper parameters.
What is M₇C₃ carbide and why does it matter?
M₇C₃ is a hard, isolated rod-shaped chromium carbide that forms in high-chrome cast iron after proper heat treatment. The brittle network M₃C carbide (found in ordinary cast iron) creates a continuous crack path; the isolated M₇C₃ rods interrupt that path, giving high-chrome cast iron both high hardness and adequate toughness. Huasuma confirms M₇C₃ morphology by metallographic analysis on every piece.
Which 2PG crusher models are compatible?
Segments are compatible with 2PG-400, 2PG-610, 2PG-750 and 2PG-900 series double roll crushers. Roll diameter, roll length and shaft bore dimensions can be custom-machined to customer drawings for any 2PG model or non-standard roll crusher.
Huasuma is a Chinese manufacturer of double roll crusher segments in high-chrome white cast iron (KmTBCr15, KmTBCr20, KmTBCr26) for 2PG series double roll crushers. HRC 58–65, 1.5 times the life of manganese steel. Supplied worldwide. Request a quote or sample.